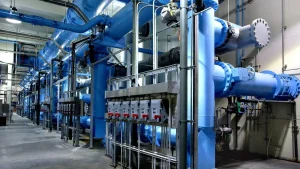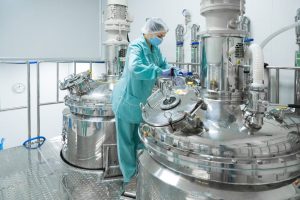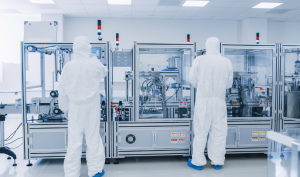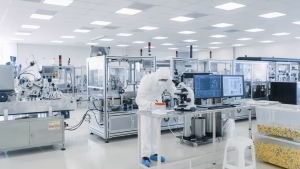
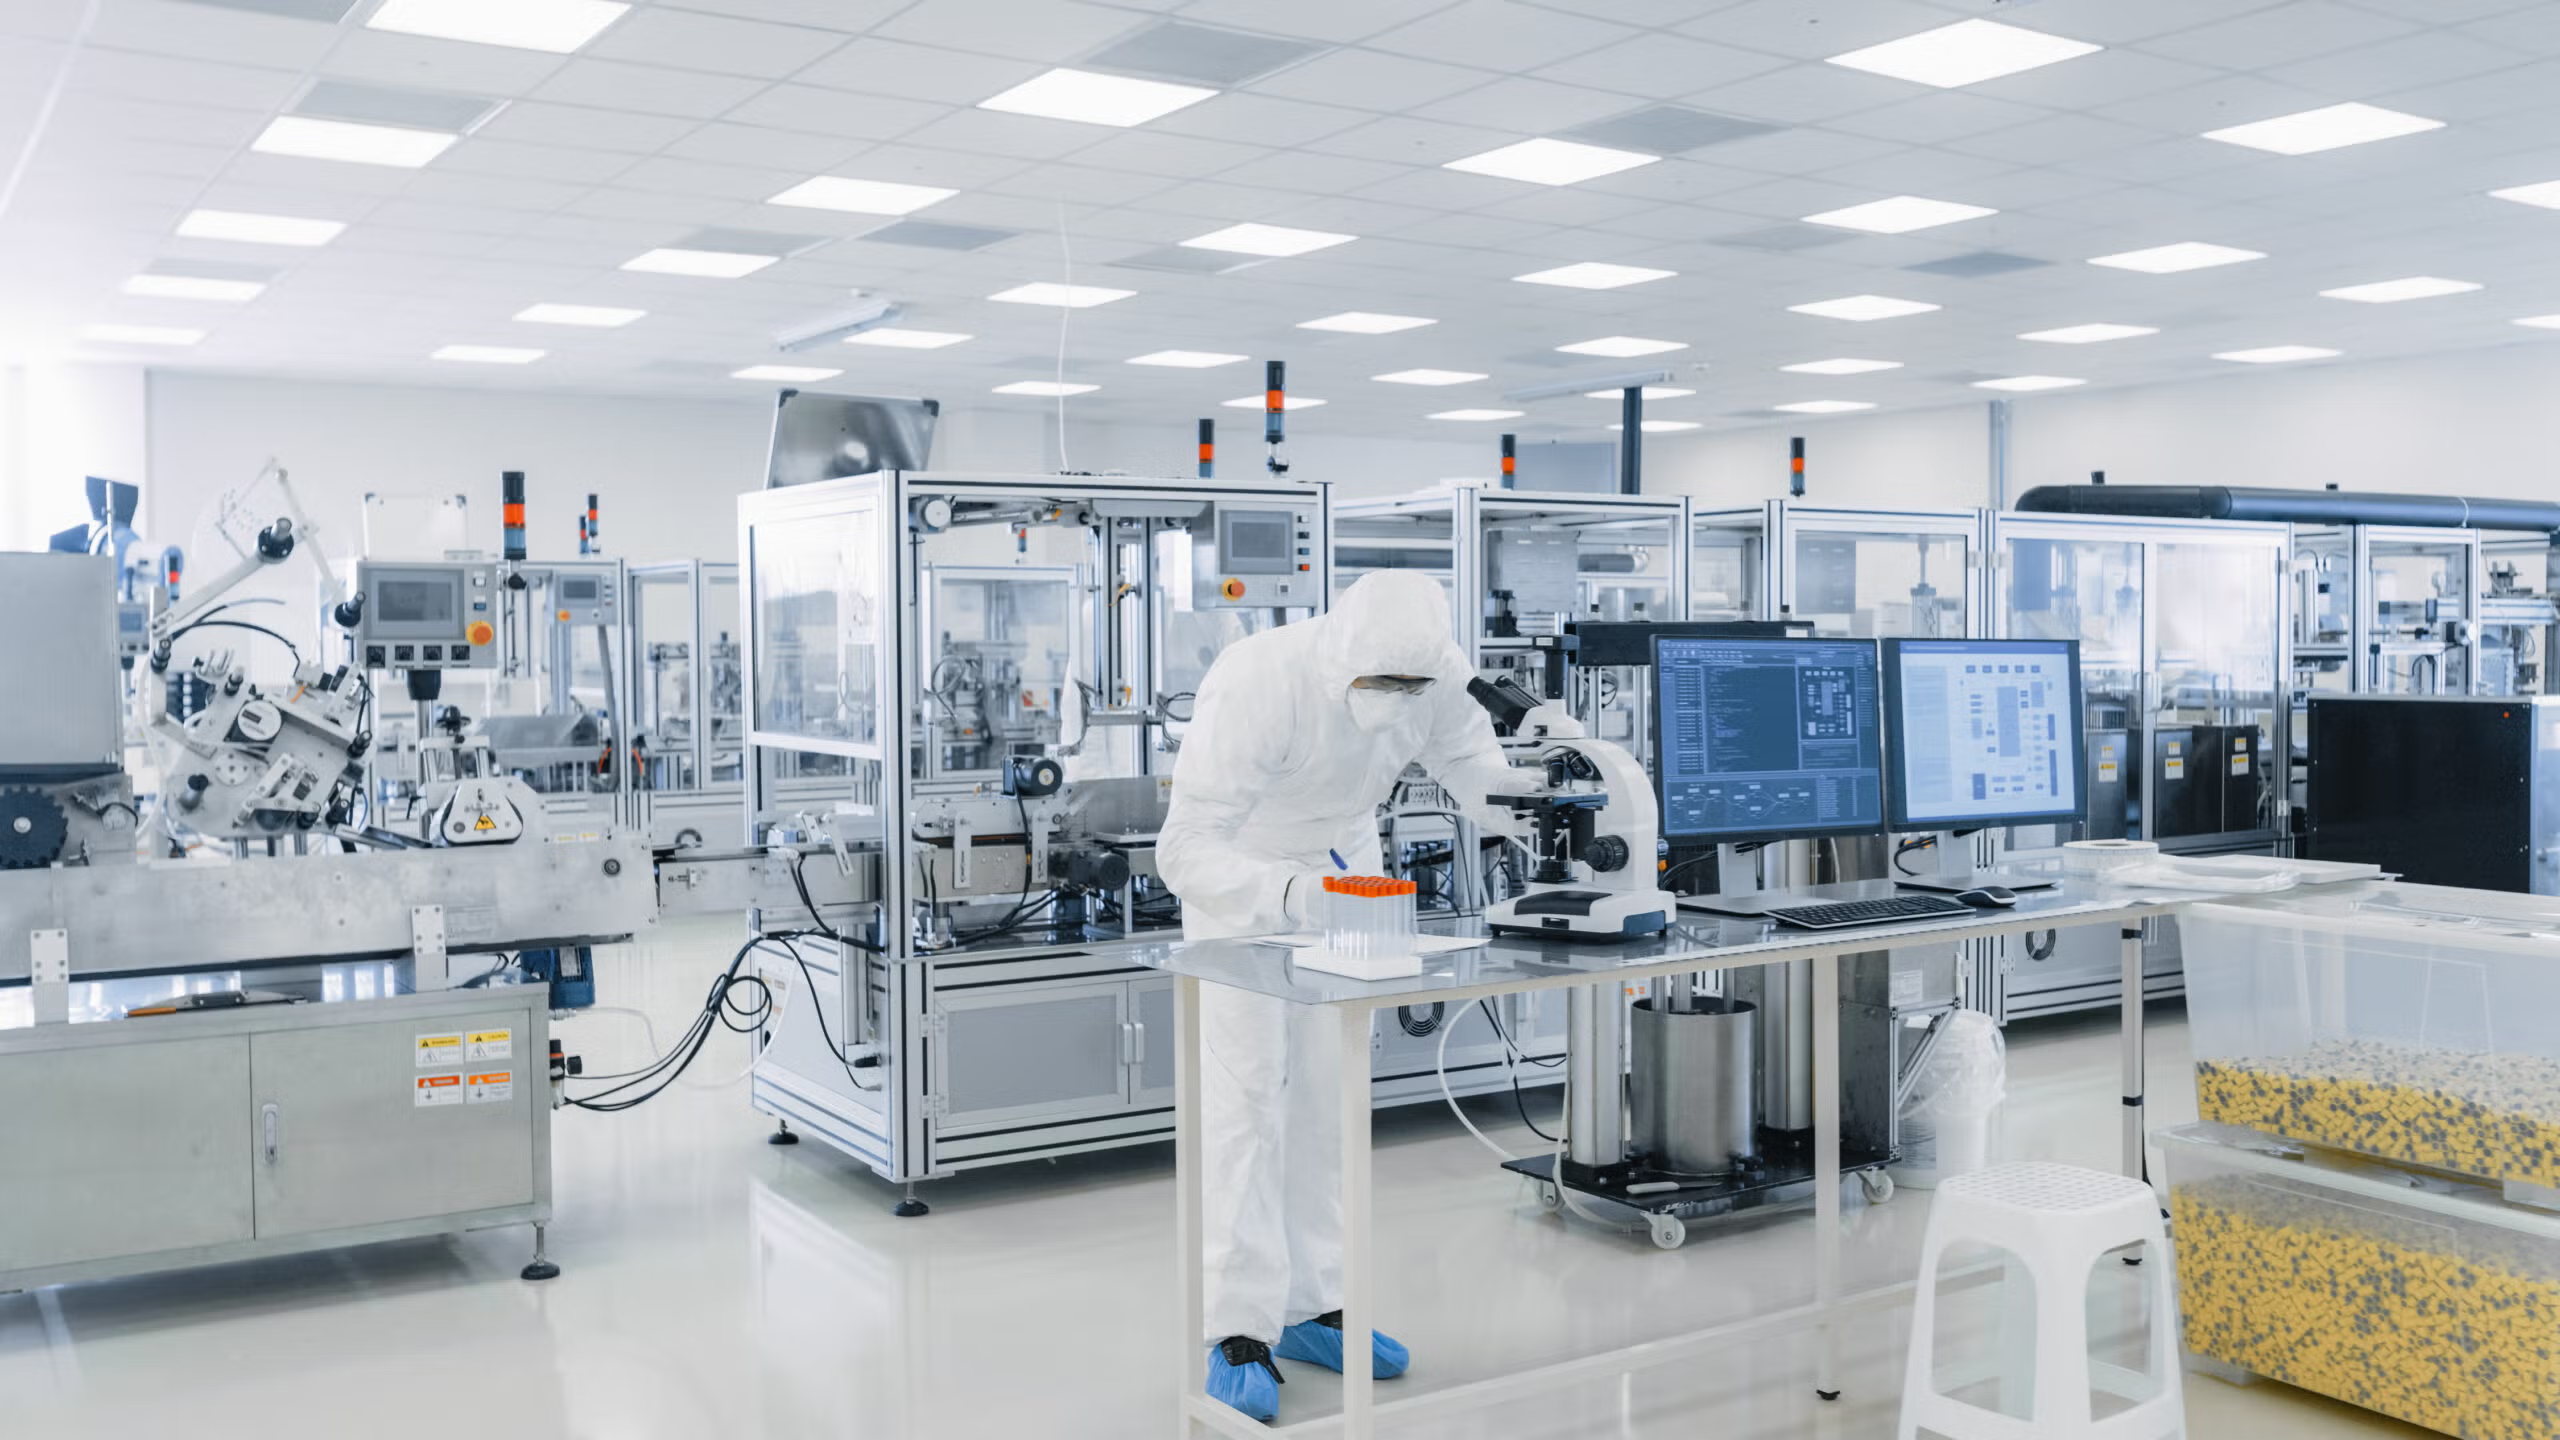
In the pharmaceutical industry, which is strictly regulated by national and international standards such as GMP (Good Manufacturing Practice), facility design is not merely about physical appearance, but serves as a fundamental foundation for production effectiveness and safety. Pharmaceutical facility design optimization is a crucial element in ensuring operational efficiency, smooth production flow, and regulatory compliance.
Why Is Facility Design So Important?
Good pharmaceutical facility design helps companies to:
-
Minimize the risk of cross-contamination
-
Optimize material and personnel flow
-
Improve productivity and operational efficiency
-
Reduce long-term operational costs
-
Ensure compliance with regulatory audits and certifications
Poor design can have a significant impact on product quality and patient safety.
Amidef’s Role in Pharmaceutical Consulting & Design
As a provider of engineering and pharmaceutical design solutions, Amidef Rekatehnik Indonesia offers comprehensive services ranging from initial consultation, layout design, to installation and production system validation.
Key approaches include:
-
Efficient process flow design: separating clean and dirty areas, minimizing the crossing of raw materials and finished products
-
Proper cleanroom and HVAC system implementation
-
Integration of automation systems to improve production efficiency
-
Selection of building materials and finishes that comply with GMP regulations
Brief Case Study
One of Amidef’s clients achieved up to a 30% increase in production efficiency after redesigning the production area and installing an ISO Class 8 HVAC system for the mixing room. In addition, facility validation and certification processes were completed smoothly due to complete and well-structured documentation.
Steps Toward Optimal Pharmaceutical Design
-
Consultation and Needs Analysis – Aligning design with product type, production capacity, and applicable regulations
-
Layout Planning – Organizing zones such as raw materials, mixing, packaging, quarantine, etc.
-
Selection of Supporting Systems – Clean air, HVAC, lighting, and finishing materials
-
Installation and Construction Supervision – Executed by experienced technical teams
-
Documentation and Validation (IQ/OQ) – Essential for audits and production licensing
Conclusion
In the highly competitive and strictly regulated pharmaceutical industry, facility design is not an area that can be overlooked. With Amidef, pharmaceutical companies can build efficient, safe, and fully compliant production facilities. Through a systematic approach and deep expertise, pharmaceutical design optimization is no longer just a concept, but a real investment in the future of reliable drug production.
Looking for a free consultation on your pharmaceutical facility design?
Get in touch with Amidef Rekatehnik Indonesia today and receive solutions that are fully aligned with your requirements and industry standards.